Professional cable manufacturer
Professional cable manufacturer
Home » Products » Cable Accessories » Custom Wire Harness & Cable Assembly — Build-to-Print
Cut, strip, crimp and assemble to your drawing — PV harnesses with MC4-type connectors, control-cabinet harnesses and low-voltage equipment wiring, built to IPC/WHMA-A-620 Class 2 workmanship with 100% continuity and polarity checks.

What a harness programme is judged on: the drawing, the workmanship class, the inspection regime and where the rating comes from.
This page is about build-to-print work: you send a drawing, a sample or a connector set, and we cut, strip, crimp, mark and assemble the harness, then test it before it ships. It is the service behind the pre-terminated products elsewhere on this site — the same process, applied to your configuration.
The workmanship basis is IPC/WHMA-A-620 Class 2, the class written for dedicated-service electronic assemblies. That fixes how terminations, wire routing, strain relief, marking and inspection are judged. Crimp connections are made with a controlled crimping process: the tool, the strip length and the crimp height are set and verified on the first article, and then held for the run.
There are three families of work: photovoltaic DC harnesses with MC4-type connectors, industrial harnesses for control cabinets, sensors and valve islands, and low-voltage harnesses for vehicles and mobile equipment. Only the photovoltaic family has published ratings on this page, because those are the values we can support with our own connector and cable data. For the other two families we quote to your drawing and the materials you specify.
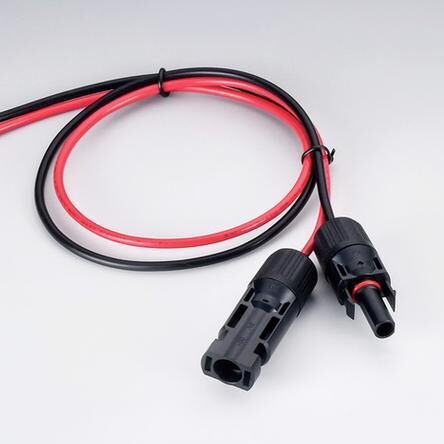
For PV assemblies the numbers are set by the connector, not by the cable: the assembly is rated at 30 A continuous / 50 A peak and −40°C to +85°C, both taken as the lower of the cable and the connector. The connector is an IEC 62852 compliant MC4-type pair, IP68 when mated — the full connector data, including voltage ratings and test values, is published on our MC4 connector and pre-terminated harness page.
Two honest limits. First, we do not claim cross-brand interchangeability: our connectors use the standard Ø 4 mm MC4-type interface, but mating them with another manufacturer's connector is not claimed and is not the basis on which the assembly is supplied. Second, we make no automotive qualification claims — if your drawing cites automotive cable or system standards, we build to the drawing and the specified materials, and we say so plainly rather than implying a qualification we do not hold.
More about the manufacturer: About SORIVO →
We assemble to your drawing, your sample or your connector set — the construction is fixed by your document, not by us.
Workmanship and acceptance follow the Class 2 requirements for dedicated-service assemblies.
Tooling, strip length and crimp height are set for the terminal and verified on the first article before the bulk run.
Every assembly is continuity and polarity checked; connector pull force is verified on a sampling basis.
Samples are submitted with inspection records so the assembly is signed off before production starts.
4 mm² standard and 6 mm² on request (AWG 12 / AWG 10), rated 30 A continuous and −40°C to +85°C.
The assembly is rated by the lower of cable and connector; the conductor ampacity is never presented as the assembly rating.
Inspection records, test records and declarations issued with the shipment; RoHS and REACH statements per order.
Photovoltaic, industrial and low-voltage — with the published data where we have it and your drawing where we do not.
Module jumpers and pre-terminated leads with MC4-type connectors on H1Z2Z2-K solar cable.
Pre-terminated DC leads for combiners, string inverters and central inverters, to specified lengths.
Panel-internal harnesses, terminal crimping, ferrules, wire numbering and bundling to drawing.
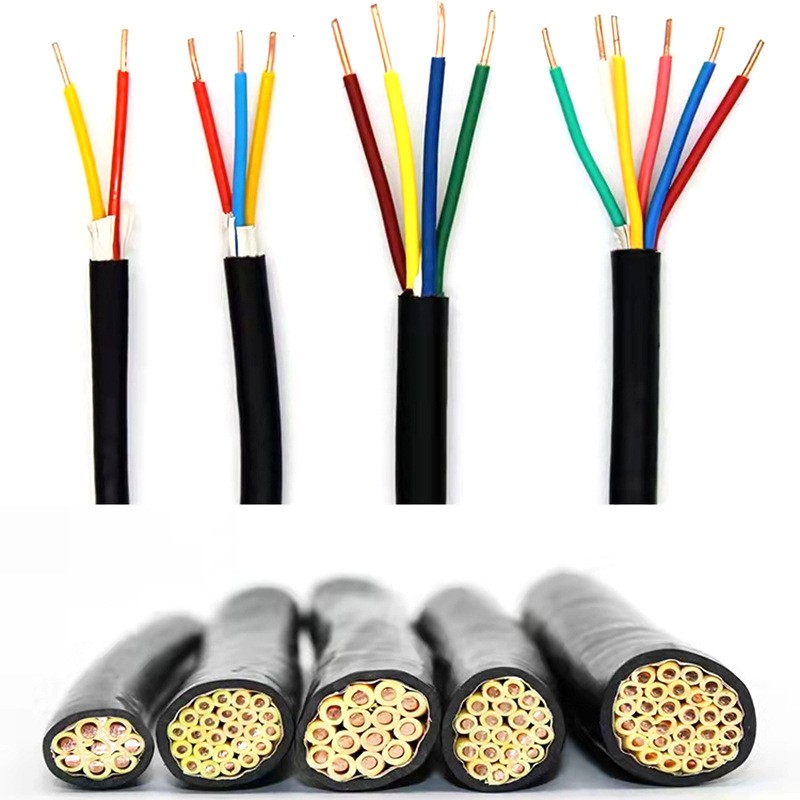
Multi-core sensor leads and valve-island harnesses assembled to the customer drawing and pinout.
Internal wiring sets for machines and packaged equipment, cut to length with ferrules and marking.
Low-voltage interconnect leads for racks, containers and DC distribution, built to the specified terminals.
Low-voltage harnesses for vehicles and mobile equipment, processed to the customer drawing and materials.
Small first-article and pilot batches to prove a design before tooling and volume release.
Published values apply to the photovoltaic assemblies; industrial and low-voltage harnesses are quoted to your drawing.
| Application | Conductor range | Connector / termination | Rating basis |
|---|---|---|---|
| Photovoltaic DC modules, strings, combiners, inverters | H1Z2Z2-K single core — 4 mm² standard, 6 mm² on request (AWG 12 / AWG 10) | Sorivo MC4-type connector pair, Ø 4 mm male / female | Lower of cable and connector 30 A continuous / 50 A peak · −40°C to +85°C |
| Industrial equipment control cabinets, sensors, valve islands | To drawing and specified material | To drawing — terminals, ferrules and connectors as specified | Lower of the selected cable and connector, confirmed with the quotation |
| Vehicle & mobile equipment low-voltage wiring | To drawing and specified material | To drawing — terminals and connectors as specified | Lower of the selected cable and connector, confirmed with the quotation |
The photovoltaic row is the only family with published ratings, because those are the values supported by our own connector and cable data. For industrial and low-voltage harnesses the conductor, connector and rating are fixed by the customer drawing and the materials specified in it — we deliberately do not publish a range we cannot support. Assembly ratings are always taken as the lower of the cable and the connector: a 4 mm² PV cable carries 55 A in free air at 60°C ambient, but the finished assembly is rated 30 A continuous because that is the connector limit.
| General Information | |
| Service | Custom wire harness and cable assembly — build-to-print |
| Workmanship Standard | Manufactured to IPC/WHMA-A-620 Class 2 workmanship and acceptance requirements |
| Connector Standard | Crimp connections made in accordance with UL 486A-486B (Wire Connectors) |
| Inputs Accepted | Drawing (PDF / DWG / STEP), physical sample, or connector set supplied by the customer |
| Rating Rule | Assembly current and temperature are the lower of the cable and the connector |
| Marking | Wire numbering, ferrules, labels and heat-shrink marking to drawing |
| Photovoltaic Assemblies | |
| Cable | H1Z2Z2-K single-core solar cable — EN 50618:2014 / IEC 62930; Class 5 tinned copper to EN/IEC 60228 |
| Conductor Sizes | 4 mm² standard; 6 mm² on request (AWG 12 / AWG 10) |
| Connector | Sorivo MC4-type connector pair, Ø 4 mm contact system, IEC 62852 compliant |
| Assembly Rated Current | 30 A continuous / 50 A peak — the lower of cable and connector, so the connector sets the limit |
| Assembly Rated Temperature | −40°C to +85°C (connector limit; the cable itself is rated −40°C to +90°C) |
| Connector Data | Voltage ratings, test voltages, contact resistance and ingress protection are published on the MC4 connector and pre-terminated harness page rather than repeated here |
| Example Forms | Module jumpers, string leads, combiner-box jumpers, pre-terminated harnesses to specified lengths |
| Industrial & Low-Voltage Assemblies | |
| Scope | Control-cabinet harnesses, sensor and valve-island leads, machine wiring sets, low-voltage vehicle harnesses |
| Conductor & Connector | As per customer drawing and specified materials — confirmed at quotation |
| Rating | Lower of the selected cable and connector; confirmed at quotation |
| Processes | Cutting, stripping, crimping, tinning where specified, terminal insertion and locking check, marking, bundling and branch breakout, shield and earth termination |
| Quality & Inspection | |
| First Article | Sample assemblies with inspection records, submitted for written approval before bulk production |
| Routine Testing | 100% continuity and polarity check on every assembly |
| Pull Force | Verified on a sampling basis using the parameters set for the specified terminal |
| Documentation | Inspection and test records with the shipment; RoHS / REACH statements issued per order |
| Declaration of Conformity | CE marking as applicable; declaration of conformity available on request |
| Commercial | |
| MOQ | 100 pcs for standard PV pre-terminated harnesses; custom assemblies quoted per drawing |
| Lead Time | 5–10 working days for standard PV pre-terminated harnesses; custom assemblies confirmed after drawing review |
| Quotation Basis | Quotation is issued against the approved drawing revision, with MOQ, packing and lead time confirmed at that point |
| Packaging | Bags, cartons or reel-packed by part number; labelling to drawing or customer standard |
Ratings apply to the connector and cable as published: the finished assembly is always limited to the lower of the two, so the assembly figure — not the conductor ampacity — is the number to design to. Our connectors use the standard Ø 4 mm MC4-type interface, but cross-brand mating with another manufacturer's connector is not claimed; MC4 is a registered trademark of Stäubli. Industrial and low-voltage harnesses are built to the customer drawing and the specified materials; where a drawing cites an industry or automotive standard, the assembly is executed to that drawing rather than presented as a qualification held by Sorivo.
Workmanship and acceptance for the harness build follow the Class 2 requirements for dedicated-service assemblies — covering terminations, routing, strain relief, marking and inspection.
Request workmanship statement →Crimp connections are made in accordance with UL 486A-486B, the wire connector standard. This applies to the connectors and terminations, not to the harness as a certified finished product.
Request connector documents →The photovoltaic assemblies combine an IEC 62852 compliant MC4-type connector with H1Z2Z2-K cable to EN 50618 and IEC 62930. Certificates and test reports are supplied with the quotation.
Request PV documents →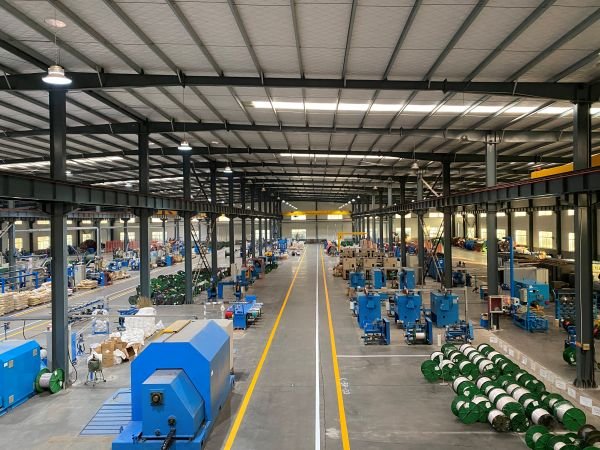
Every harness follows the same route through the workshop: review the drawing, fix the process, approve the first article, then produce and test.
Send the drawing, sample or connector set — we check readability and list the points to clarify.
We review manufacturability, tolerances, marking and materials, then quote against the approved revision.
Sample assemblies with inspection records, submitted for your written approval.
Tooling and process parameters locked to the part number, with 100% continuity and polarity testing.
Packed by part number, shipped with inspection and test records.
Send the drawing or sample — we review it and come back with the points to confirm.
The more complete the drawing package, the faster and more accurate our quotation. Our engineers reply within one working day.
Thanks — our engineers will reply within one working day.